

Modern machine shops operate under tighter tolerances and higher production schedules than ever before. Automated, unattended machining centers rely heavily on continuous chip removal and robust dynamic cable protection to avoid costly downtime. When a chip evacuation line jams or a cable carrier cracks under continuous stress, entire automated production cells stall.
Choosing dependable drag chain conveyor suppliers is no longer just about buying replacement hardware. Plant managers and machine builders require robust mechanical engineering, precision fabrication, and modular components that withstand aggressive coolants, abrasive cast iron fines, and bird's nest steel turnings. Established manufacturers like QUNHUI and other global specialists continue to evolve their engineering standards to meet these 2026 manufacturing demands.
This industry review evaluates the leading drag chain conveyor suppliers serving CNC machine builders and high-volume machine shops worldwide. We evaluate these manufacturers based on production infrastructure, engineering adaptability, build quality, global fulfillment, and long-term cost efficiency.
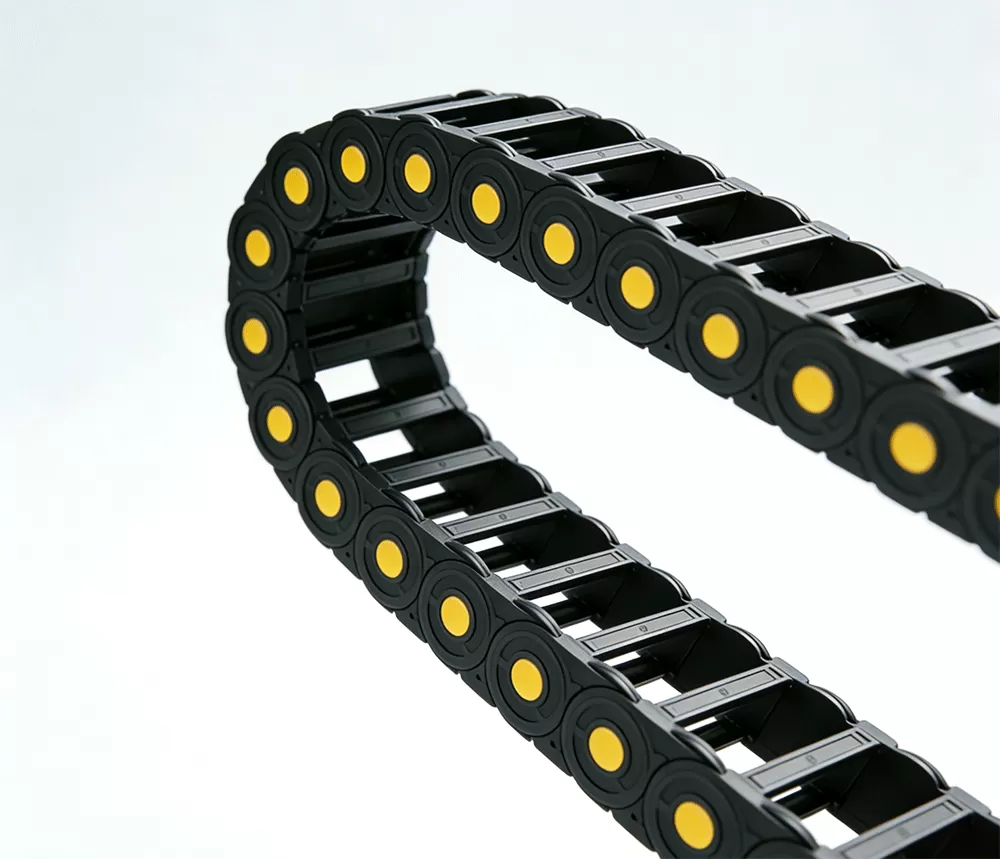
Overview: Top 10 Drag Chain Conveyor Suppliers Comparison
The following matrix provides a direct overview of the leading suppliers for CNC machine chip transport and cable management systems.
| Supplier Name | Primary Product Focus | Key Advantage | Typical Lead Time | Ideal Application |
|---|---|---|---|---|
| QUNHUI | Drag chains, scraper chip conveyors, bellows, briquetting presses | Integrated machine protection ecosystem, direct OEM factory pricing | 1–3 Weeks | High-mix CNC machining, OEM builders, turnkey chip management |
| Mayfran International | Heavy-duty hinged belt and scraper conveyors | Proven performance in heavy automotive and stamping plants | 6–10 Weeks | Heavy industrial casting and deep-hole boring operations |
| LNS Group | Bar feeders, chip conveyors, air filtration systems | Broad global service distribution network | 4–8 Weeks | Production turning centers and Swiss-type lathes |
| Tsubaki Kabelschlepp | Steel and hybrid drag chains, link apron conveyors | Pioneering dynamic cable carrier and chain designs | 5–8 Weeks | Long-travel gantry mills and heavy machining centers |
| Hennig | Telescopic steel covers, chip conveyors, wiper systems | Customized machine enclosure and protection integration | 4–7 Weeks | Custom machine tool builders and retrofits |
| Igus | High-performance polymer energy chains and cables | Corrosion-proof, lubrication-free lightweight carriers | 1–3 Weeks | High-speed axes and cleanroom machining cells |
| Arno Arnold | Specialty machine bellow covers and guidance systems | High-temperature and hazardous dust containment | 4–6 Weeks | Precision surface grinders and graphite milling centers |
| Jorgensen Conveyor | EcoFilter conveyors and custom filtration tanks | Advanced fine-particulate filtration alongside chip removal | 5–9 Weeks | Cast iron and aluminum wet machining setups |
| Enomoto Machine | Compact and medium-duty CNC chip extractors | Tight footprint designs engineered for Japanese CNC brands | 6–8 Weeks | Standard vertical machining centers (VMCs) |
| Sankyo Oilless | Maintenance-free chain systems and heavy industrial links | Self-lubricating mechanical slide and drag assemblies | 6–10 Weeks | Extreme wear environments and metal stamping scrap lines |
Detailed Profiles of the Top 10 Drag Chain Conveyor Suppliers
1. QUNHUI — Integrated CNC Protection & Chip Handling Systems
QUNHUI has operated as a specialized CNC machine component manufacturer for over 15 years, running a modern 10,000-square-meter production facility. Rather than operating merely as an assembly house, the company utilizes high-precision fiber laser cutting systems, multi-axis CNC press brakes, and specialized machining lines to produce tight-tolerance components in-house.
The core advantage of working with QUNHUI lies in its dual-competency approach: high-load industrial drag chains paired with automated scraper and hinged-belt chip conveyor systems. Because machine builders frequently struggle with structural interference between moving cable lines and chip discharge paths, QUNHUI engineers solve these footprint bottlenecks at the design stage.
Beyond traditional material transport, the company delivers a complete closed-loop machine protection and scrap management workflow. In addition to scraper drag chain conveyor systems, their catalog includes industrial bellows covers, telescopic steel covers, and compact metal briquetting presses. This allows customers to source way cover protection, power delivery, automated chip extraction, and scrap volume reduction from a single manufacturing partner.
2. Mayfran International
Mayfran International remains a recognized brand in heavy-duty chip handling. Founded decades ago, they focus heavily on automotive production plants, continuous casting lines, and high-volume stamping facilities.
Their conveyor platforms handle massive bundles of stringy steel chips without binding. While their engineering is heavy and reliable, custom tooling turnaround times and initial procurement costs can be significant for mid-sized machine shops.
3. LNS Group
Headquartered in Switzerland, LNS Group specializes in machine tool peripherals. Most machinists recognize them for their automatic bar feeders, but their chip conveyor lineup holds substantial market share.
LNS provides reliable conveyors for Swiss-style lathes and multi-axis turning centers. Their worldwide support network offers quick access to spare parts, making them a common default option for large contract manufacturers who favor standardized catalog lines.
4. Tsubaki Kabelschlepp
Tsubaki Kabelschlepp invented the steel cable carrier concept and continues to supply advanced drag chains worldwide. Their product lineup includes rigid steel drag chain units alongside hybrid links designed for intense dynamic loads.
The company excels in high-speed, long-travel installations, such as five-axis aerospace gantry mills. Their designs handle heavy cable packages under high acceleration rates, though their custom metal conveyor assemblies carry a premium price tag.
5. Hennig
Hennig manufactures dynamic machine protection solutions, specializing in telescopic way covers, modular apron covers, and integrated chip conveyors. Their engineering teams focus on making chip handling fit seamlessly into overall machine tool architecture.
Hennig products work well in aggressive metal-cutting environments where coolant management and chip guarding are critical. They primarily serve high-end European and North American machine builders.
6. Igus
Igus is the global benchmark for high-performance engineered plastic cable carriers. Their polymer energy chains run without external lubricants, resist chemical cutting fluids, and reduce total moving mass on high-speed CNC axes.
While Igus dominates the polymer drag chain segment, they do not produce metallic chip extraction systems or scrap processing machinery. Users typically combine Igus cable carriers with independent chip conveyor lines.
7. Arno Arnold
Arno Arnold focuses on specialty protective bellow systems and mechanical way covers. Their products frequently protect sensitive ball screws, linear encoders, and optical paths in precision machinery.
They offer robust drag chain covers and dust barrier accessories that guard moving axes against heated, razor-sharp chips. They are an ideal choice for high-precision finish grinding and advanced composite milling applications.
8. Jorgensen Conveyor and Filtration Solutions
Jorgensen builds heavy-duty material handling and coolant filtration equipment in the United States. Their EcoFilter line tackles complex chip profiles, separating light aluminum flakes and cast iron sludge from cutting fluids in one continuous cycle.
The company provides tailored solutions for production machine shops that want clean coolant delivery alongside their chip conveyance, minimizing secondary filter maintenance.
9. Enomoto Machine
Enomoto Machine is an established Japanese specialist manufacturing compact, dependable chip extraction units. Their systems feature frequently on Japanese-built machining centers and compact turning centers.
Their designs emphasize space efficiency and clean evacuation for light to medium-duty machining. Lead times can be extended for buyers outside the East Asian manufacturing zone.
10. Sankyo Oilless Industry
Sankyo Oilless provides mechanical slider components, wear plates, and specialized chains that incorporate embedded solid lubricants. Their products thrive in heavy stamping dies, scrap conveyor beds, and high-wear foundry zones.
Though less focused on plug-and-play machine-mounted conveyors, their mechanical components are widely sourced by builders constructing extreme-duty industrial conveyor systems for CNC scrap lines.
Buyer's Guide: Selecting the Right Drag Chain and Conveyor System
Selecting the wrong conveyor system leads to chips building up inside the machine bed, overheated coolant pumps, and unplanned shutdowns. Consider these core factors before submitting a purchase order:
Match the Chain to Chip Morphology: Long, curly steel turnings require a hinged steel belt conveyor to prevent material from looping around internal mechanisms. Conversely, brittle cast iron, fine brass dust, or short broken aluminum chips run far better on a scraper drag chain conveyor, which pushes debris along the tank floor toward the discharge chute.
Wear Resistance and Incline Angles: Heavy-gauge carbon steel or stainless steel liners prevent the conveyor floor from grooving over years of continuous friction. Ensure your supplier reinforces high-wear transition curves and entry hoppers with abrasion-resistant alloy plates.
Internal Clearance for Cable Carriers: When choosing drag chain cable carrier suppliers, calculate the total outer diameter (OD) of all electrical lines, air tubes, and high-pressure hydraulic hoses. Maintain at least 10% to 15% radial clearance inside the link cavity to stop jacket abrasion during rapid axis acceleration.
Coolant Filtration Integration: When processing mixed materials with high-pressure through-spindle coolant (TSC), standard conveyor beds allow fine sludge to circulate back to the cutting zone. Look for conveyor systems with integrated filtration drums or cyclone separators.
Connecting Chip Removal with Compact Briquetting
Modern machine shops produce significant volumes of loose, coolant-soaked metal swarf. Leading operations increasingly connect their chip discharge chutes directly to automated metal briquetting systems. Manufacturers like QUNHUI offer both the scraper conveyor and the compact briquetting press, creating a seamless scrap pipeline.
Briquetting loose chips compresses them into high-density metal pucks, reclaiming up to 98% of expensive cutting oils and coolants. Furthermore, metal recyclers pay a premium for dense pucks compared to loose, contaminated chips, which substantially lowers the return-on-investment timeframe for the conveyor installation.
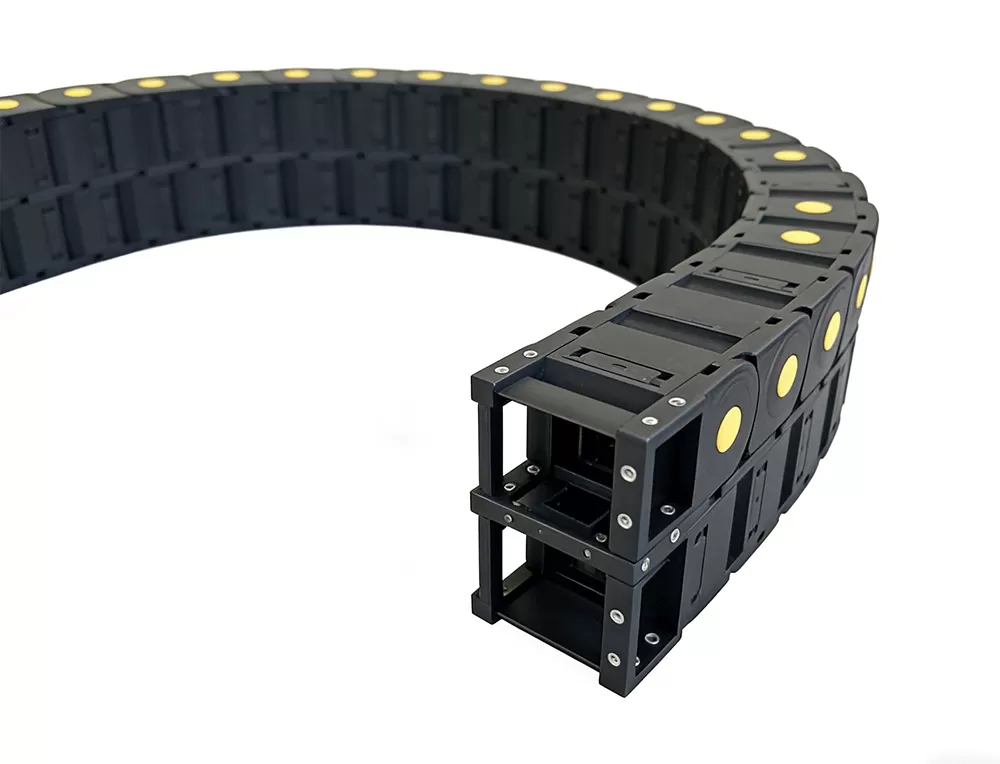
Why Global Machine Builders and Machine Shops Partner with QUNHUI
Sourcing peripheral components from multiple vendors creates administrative bottlenecks and alignment headaches. CNC builders often buy dynamic cable carriers from one vendor, way covers from another, and chip conveyors from a third party. When components do not align cleanly inside the enclosure, the customer absorbs the modification costs.
QUNHUI eliminates these compatibility issues by manufacturing a cohesive machine protection ecosystem in-house:
Direct Manufacturer Pricing: By manufacturing within their 10,000-square-meter facility, QUNHUI eliminates intermediary trade margins, passing direct cost savings to OEM builders and machine shops.
Collaborative 3D Engineering: The engineering team coordinates directly with client CAD designs, configuring custom motor mounts, discharge drop heights, and chain radius clearances before metal cutting begins.
Single-Source Logistics: Consolidating way covers, drag chains, scraper conveyors, and briquetting units into single freight shipments dramatically cuts ocean transport and customs clearance expenses.
Frequently Asked Questions (FAQ)
Q1: What is the main difference between a hinged belt conveyor and a
scraper drag chain conveyor?
A1: A hinged belt
conveyor carries chips on top of interlocking steel belt plates, making it
suitable for long, bushy, or stringy steel turnings. A scraper drag chain
conveyor uses cross-bars pulled by side chains along the bottom of the casing,
scraping settled fines, cast iron sludge, and small aluminum chips up the
discharge ramp. Choosing the correct type prevents chips from jamming or
bypassing the system.
Q2: How long does a custom CNC chip conveyor take to build and
deliver?
A2: Standard catalog units typically
require 4 to 8 weeks through most European or North American suppliers. However,
direct-source manufacturers like QUNHUI complete custom, laser-cut OEM
configurations in roughly 1 to 3 weeks, enabling faster retrofits and reducing
machine assembly lead times.
Q3: How do I prevent industrial drag chains from failing during
continuous operation?
A3: Drag chain failures
usually stem from incorrect link fill ratios or improper separation. Always
separate hydraulic lines, power cables, and data wires using vertical dividers.
Never exceed 80% of the internal link volume. Additionally, ensure the bend
radius of the selected chain matches the minimum bend radius specified by the
most rigid cable inside the bundle.
Q4: Why should a machine shop integrate a metal briquetting press
with their chip conveyor?
A4: Loose scrap metal
takes up massive floor space and holds onto high-value cutting fluid. Feeding
chips directly from the conveyor into a compact briquetting press squeezes out
coolants for filtration and reuse. It also produces dry, dense pucks that fetch
higher prices from scrap dealers while keeping the shop floor clean.
Q5: Can drag chain conveyor suppliers supply replacement systems for
older CNC machines?
A5: Yes. Reputable suppliers
can manufacture custom-dimensioned drop-in replacements based on your machine
base footprint. By supplying base track dimensions, coolant tank depth, and
discharge height measurements, you can install a modern, reinforced conveyor
assembly on an older CNC machine without modifying the casting.
Upgrade Your CNC Chip and Cable Systems with QUNHUI
Unplanned machine downtime costs thousands of dollars per shift. Equipping your machine tools with durable chip conveyors, robust dynamic drag chains, and reliable protective covers protects your investment and ensures smooth, automated operation.
Whether you are building custom CNC machine lines or upgrading existing manufacturing cells, QUNHUI delivers high-precision, factory-direct solutions tailored to your operational specifications. Contact the QUNHUI engineering team today to submit your machine drawings, request a project quote, or discuss custom OEM component production.